
Call: 08071725018
 Send Inquiry
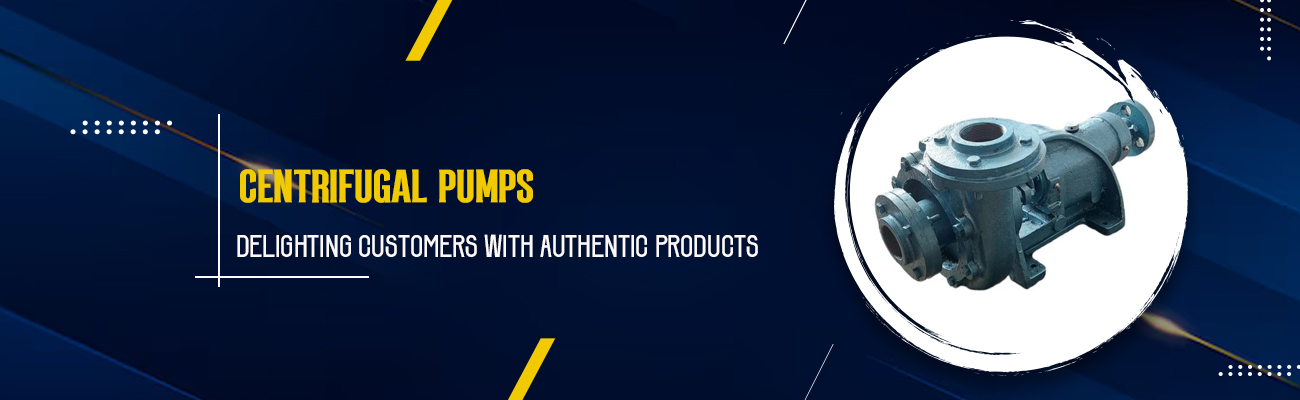
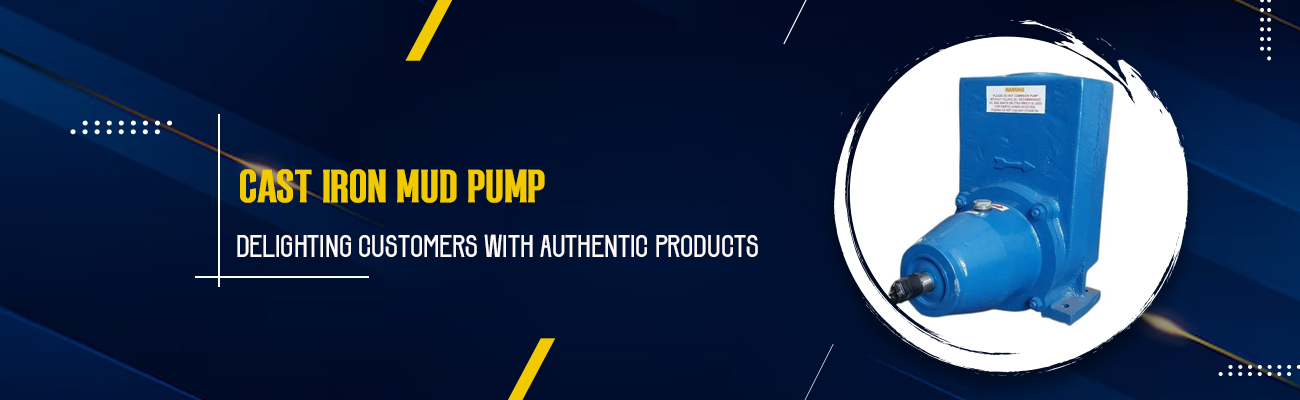
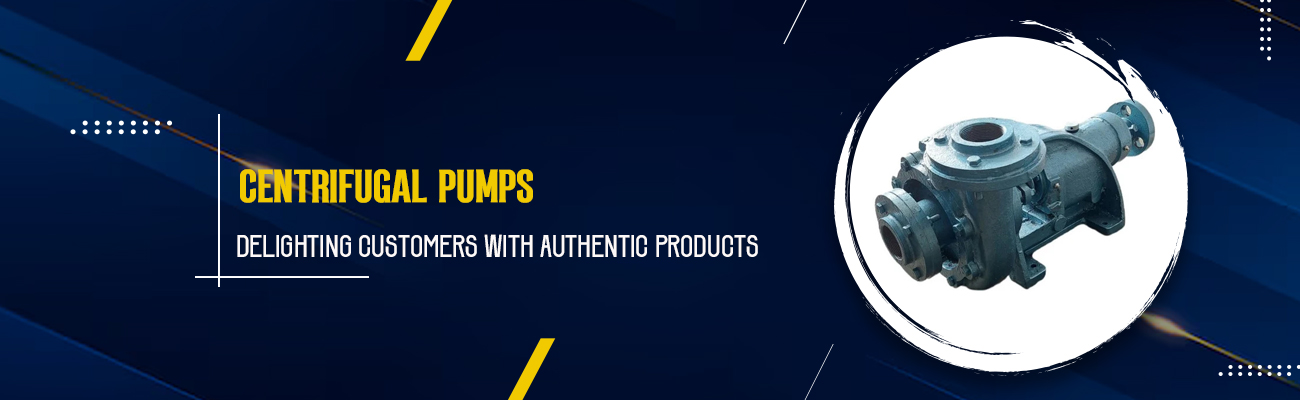
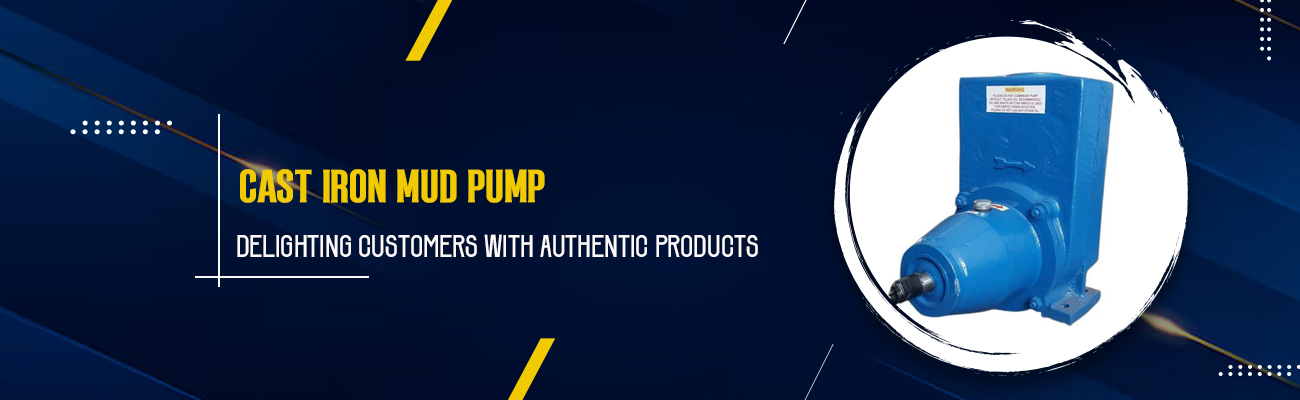
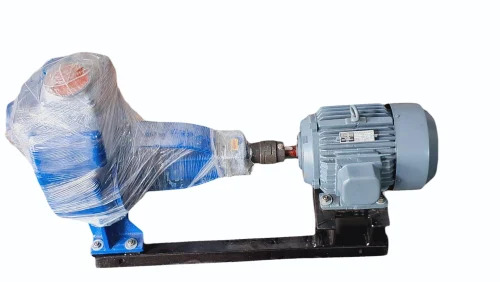
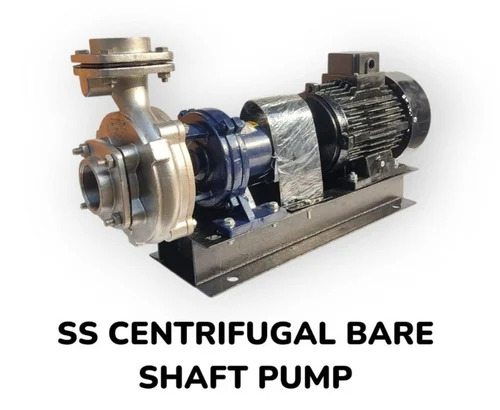
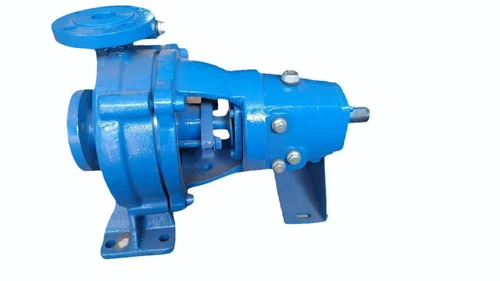
Powering industries with robust Boiler Feed Pump, Centrifugal Chemical Process Pump, Stainless Steel Centrifugal Pumps, Acid Pumps, Suction Pump, Self Priming Mud Pump, etc., engineered for efficient, reliable fluid handling.
- New Arrivals
- Featured
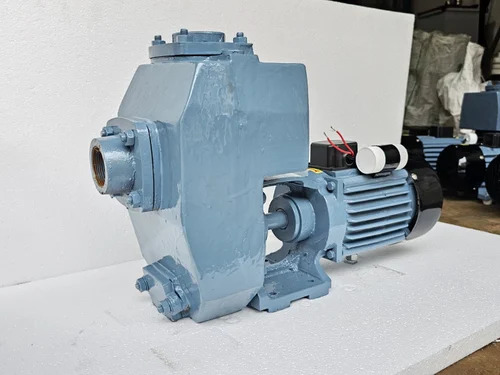
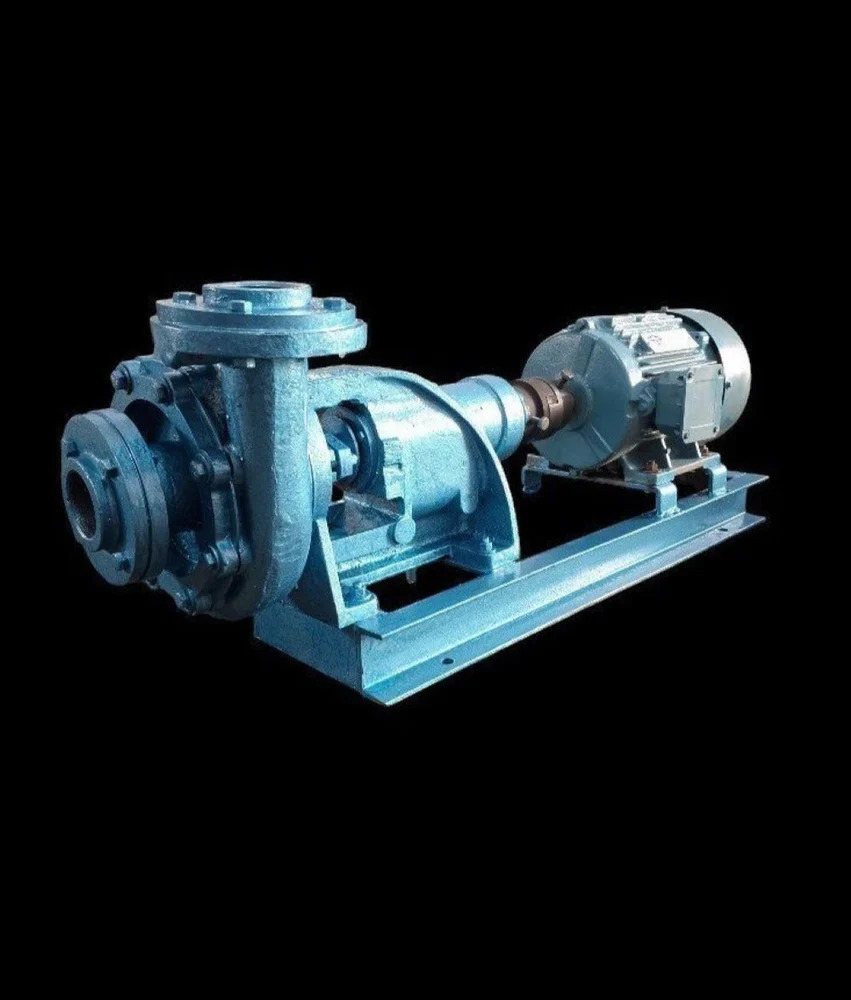
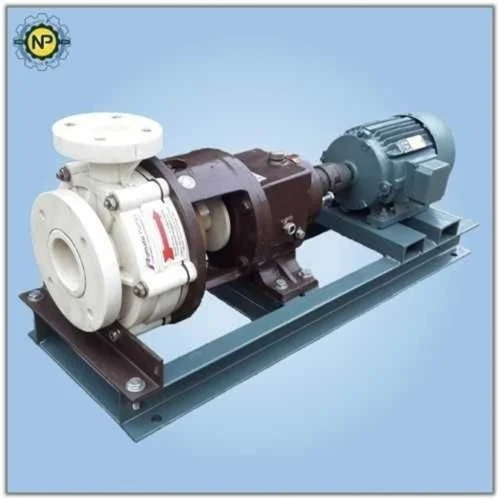
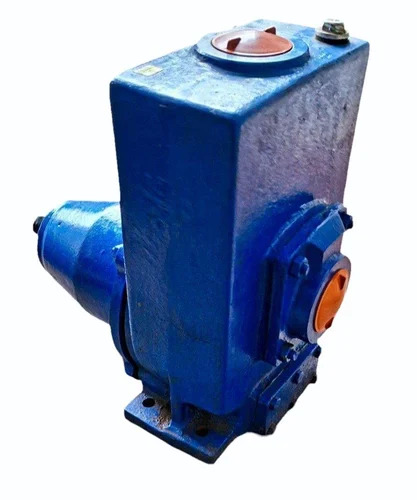
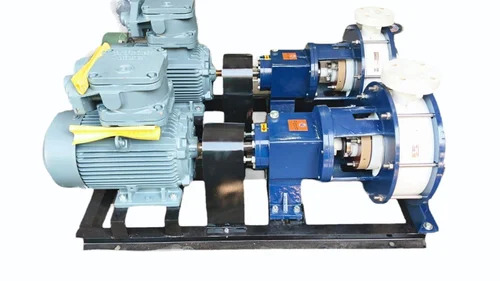
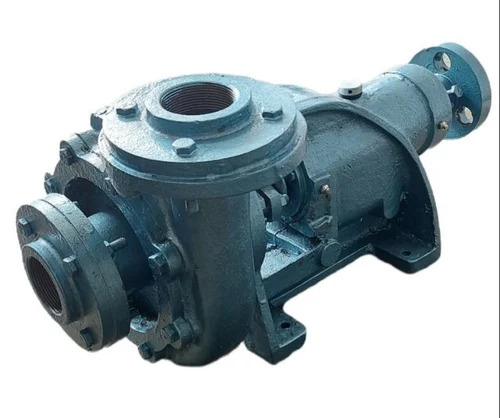
Established in 2022, Vishwakarma Engineering is an Ahmedabad, Gujarat based manufacturer, supplier and service provider specializing in dependable pumping solutions for diverse industrial fluid handling requirements. Our company offers a broad range of pumps, including Centrifugal Chemical Process Pump, Stainless Steel Centrifugal Pumps, Boiler Feed Pump, Suction Pump, Acid Pumps, Self Priming Mud Pump, and much more.
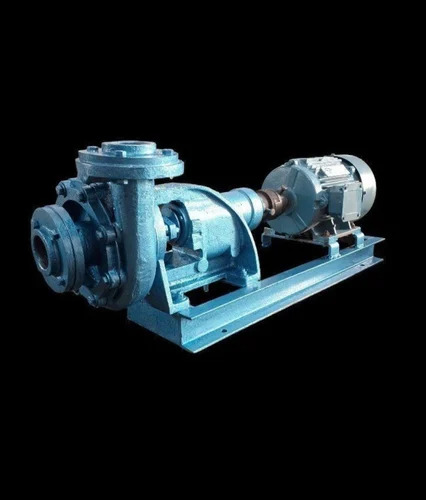
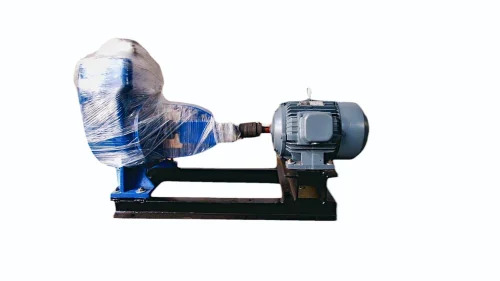
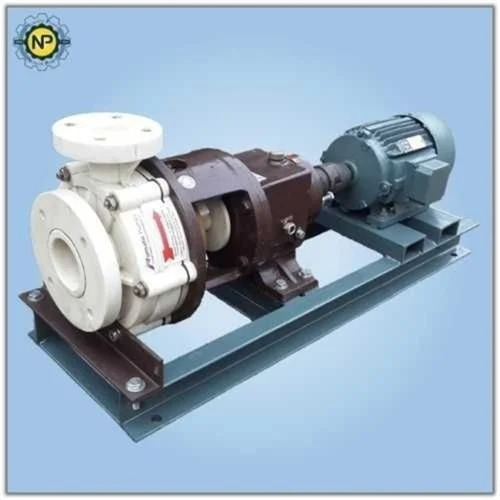
We focus on developing and supplying pumps designed for efficient liquid transfer, circulation and process applications. Its product range includes stainless steel and other material configurations selected according to application requirements. Stainless steel centrifugal pumps are offered for industries such as pharmaceuticals, food and beverage, dairy, chemicals and RO plants, while chemical and acid transfer pumps are suited to demanding fluid handling environments. Boiler feed pumps are designed for boiler feeding applications, while mud pumps support operations involving loading, unloading, circulation, washing, firefighting and related duties.
Our company emphasizes quality conscious manufacturing, suitable raw materials, skilled personnel and systematic inspection. Our experienced team works with modern manufacturing techniques and application oriented designs to maintain dependable product performance. With a customer focused approach, reasonable commercial offerings and attention to promised delivery schedules, we aim to build lasting relationships through consistent products and responsive support.
Quality Assurance
We places strong emphasis on quality assurance across its pumping solutions. Our company focuses on selecting suitable raw materials, maintaining consistent manufacturing practices and conducting systematic inspections to support reliable pump performance. Each product is developed with attention to application requirements, operating conditions and durability. Skilled professionals oversee production and quality related activities to help maintain consistent standards across the product range. This quality focused approach enables the company to supply dependable pumps for chemical, pharmaceutical, food and beverage, dairy, water treatment, RO plant and other demanding industrial applications.
Most Popular Products
Contact Details
Vishwakarma Engineering
GST : 24AFRPP5761P2ZH
- Shed No. 34, Samir Industrial Estate, B/S Ishan Dye, Phase-1, Vatva GIDC, Ahmedabad - 382445, Gujarat, India
- Phone :08071725018
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.


